Switching a machine off doesn't make it safe to service. A charged hydraulic accumulator, a compressed spring, or a coworker hitting the start button can still injure the technician working on it. Lockout/tagout (LOTO) procedures prevent that by isolating energy sources and locking it in the off position until the work is done.
This guide walks through a seven-step LOTO procedure you can adapt to your equipment, what OSHA's standard requires, and how to keep your program consistent across crews and shifts.
Key takeaways
- Lockout/tagout procedures protect technicians from unexpected startup and stored-energy release during equipment servicing.
- A standard procedure identifies energy sources, notifies affected employees, shuts down and isolates equipment, applies devices, releases stored energy, verifies isolation, and ends with a controlled release from lockout.
- OSHA’s standard, 29 CFR 1910.147, calls for an energy control program with written procedures, training, and periodic inspections. Check the applicable requirements for your facility.
- Following best practices makes your LOTO procedures more effective. Regular inspections, hands-on training, and strict enforcement help prevent complacency and OSHA violations.
- A CMMS makes LOTO procedures easier to manage and audit. It helps digitize hazardous energy control procedures, assign and track lockout tasks, and create audit trails to satisfy OSHA inspectors.
Why are LOTO procedures important?
Lockout/tagout (LOTO) procedures shut down energy sources in electrified equipment so technicians can safely perform maintenance. Having reliable, consistent LOTO procedures is key to worker safety because they:
- Prevent accidental machine startup during maintenance, ensuring employee protection
- Reduce the risk of serious injuries or fatalities
- Ensure compliance with safety regulations and OSHA standards
- Protect equipment from unintended damage during servicing
Implementation can seem tricky, especially in large facilities with diverse equipment. However, getting it right is critical for minimizing the risk of worker injuries and OSHA penalties.
This guide gives you a ready-to-use LOTO checklist, plus our tips and best practices for compliance with OSHA requirements.
Step-by-step lockout/tagout procedure
Use these seven steps to plan the work and lock out the equipment safely. OSHA’s standard sets the sequence for applying energy control; adapt each step to your machine’s written lockout/tagout procedure.
1. Preparation: Identify energy sources
Every lockout starts with knowing what powers the machine and how to control each source:
For example, a technician preparing to service a press may identify the electrical supply but miss a charged hydraulic accumulator. Check the procedure against the machine in front of you, including secondary and stored sources, before anyone turns it off.
2. Notification: Inform affected employees
Before applying a lock or tag, notify affected employees about the work:
For instance, a maintenance crew scheduling a weekend repair on a packaging line should tell the Friday operators before they leave and brief the Monday crew before startup. Anyone who wasn't told may assume the line is ready to run.
3. Shutdown: Power down equipment
Once employees know about the work, properly shut down the machine in an orderly way that doesn't create additional hazards:
A conveyor may stop while its associated hydraulic unit continues to run. Check the whole machine before moving to isolation.
4. Isolation: Disconnect energy sources
After the equipment is shut down, you need to physically cut off the equipment from the energy supply. To do it right:
Turning off a press at its control panel stops it but leaves the supply connected. OSHA doesn't treat push buttons, selector switches, or other control-circuit devices as energy-isolating devices, so isolation has to happen at the source itself.
5. Lockout/tagout: Apply devices
With every source isolated, apply lockout or tagout devices. Use lockout procedures wherever a device can accept a lock, unless the employer can show tagout provides full employee protection. When applying devices:
Use devices dedicated to energy control rather than makeshift ones, and give tags a clear warning, such as "Do Not Start."
6. Release stored energy: Ensure zero energy state
After applying locks or tags, relieve, disconnect, or restrain any stored or residual energy that could be hazardous:
For example, residual pressure in a locked-out hydraulic press can let its ram drift, so bleed the lines and block the ram before anyone reaches into the die area. Some energy can also build back up during the job, such as pressure creeping back into a line. If that could reach a hazardous level, keep verifying isolation until the work ends or reaccumulation is no longer possible.
7. Verification: Confirm isolation
As the last check before maintenance begins, clear everyone from the machine, then verify isolation and deenergization as OSHA's standard requires:
Return the controls to off after testing, as OSHA's non-mandatory Appendix A cautions. Only begin maintenance once every test confirms the equipment won't start or move.
*Disclaimer: This checklist is to be used only by those with appropriate training, expertise, and professional judgment. You are solely responsible for reviewing this checklist to ensure that it meets all professional standards and legal requirements, as well as your needs and intent.
OSHA lockout/tagout requirements
Lockout/tagout isn’t just an internal safety practice. It’s a compliance requirement.
Following OSHA’s Control of Hazardous Energy standard (29 CFR 1910.147) helps protect personnel and avoid hefty penalties. This graphic outlines the program’s parts:

OSHA has outlined various LOTO requirements. These requirements apply depending on your equipment portfolio, whether contract or temporary workers are involved in maintenance, and other factors.
If you're creating a LOTO checklist or tweaking our template, read these requirements to ensure your LOTO procedure checks all OSHA compliance boxes.
Here's what OSHA requires:
- Energy control program: Establish a program made up of energy control procedures, employee training, and periodic inspections (29 CFR 1910.147(c)(1)).
- Detailed energy control procedures: Develop, document, and use procedures outlining steps to shut down, isolate, block, secure, and verify the effectiveness of lockout or tagout safety measures for each machine or piece of equipment (29 CFR 1910.147(c)(4)(i)–(ii)).
- Training for authorized, affected, and other employees (29 CFR 1910.147(c)(7)(i)):
- Authorized employees (people who actually perform the lockout/tagout procedures) must understand how to recognize hazardous energy and apply control methods.
- Affected employees (workers who operate or use the equipment, or work in the area where it's being serviced) must understand the purpose and use of LOTO procedures.
- Other employees (anyone who works or may work in an area where LOTO procedures are used) must know not to restart or reenergize locked or tagged equipment.
- Retraining: Authorized and affected employees must be retrained when job assignments change, when a change in machines, equipment, or processes introduces a new hazard, when procedures change, or when an inspection or other evidence reveals gaps (29 CFR 1910.147(c)(7)(iii)).
- Annual periodic inspections and corrective follow-up: An authorized employee other than the one(s) using the procedure must inspect each energy control procedure at least annually to ensure compliance and correct deficiencies. The employer must certify each inspection, recording the machine, the date, the employees included, and the inspector (29 CFR 1910.147(c)(6)).
- Verification of isolation before servicing: Test the equipment before work begins (29 CFR 1910.147(d)(5)–(6)). This could include trying to start equipment, testing voltage, releasing residual energy, etc.
- Protection of contract and temporary workers: Coordinate LOTO procedures with outside contractors or temporary staff. Each employer informs the other of its procedures, and the on-site employer makes sure its employees understand and follow the outside employer's restrictions (29 CFR 1910.147(f)(2)).
- Limited exceptions: Minor tool changes, adjustments, and other minor servicing during normal production may be exempt if they're routine, repetitive, integral to production, and alternative measures provide effective protection (note to 29 CFR 1910.147(a)(2)(ii)).
Most people stop at 29 CFR 1910.147. However, LOTO requirements are sprinkled across several other OSHA standards: 29 CFR 1910.333, 29 CFR 1910.179, 29 CFR 1910.269, and 29 CFR 1910.217.
It's best to work with an internal expert and scan through applicable standards to make sure you don't miss out on any requirements. If you're a small or medium-sized business, consider contacting OSHA to sign up for their free on-site consultation program and understand all requirements.
When to run this LOTO compliance checklist
Run the full procedure when servicing or maintenance could expose someone to unexpected energization, startup, or stored energy release. Check these situations before work:
- Production work: Normal production operations fall outside the standard. Servicing during production falls within it when someone must remove or bypass a guard or place any part of the body in the point of operation or an associated danger zone during the machine’s cycle (29 CFR 1910.147(a)(2)(ii)). For example, clearing a packaging-line jam may require removing a guard; add that task to your machine guarding inspection checklist.
- Cord-and-plug equipment: The standard does not apply when unplugging controls exposure to unexpected startup, and the employee doing the work retains exclusive control of the plug (29 CFR 1910.147(a)(2)(iii)(A)).
- Equipment changes: When you install new equipment or replace, make a major repair to, renovate, or modify existing equipment, ensure its isolating devices accept a lock. Update its written procedure; retrain employees if the change introduces a new hazard (29 CFR 1910.147(c)(2)(iii), (c)(4)(i), (c)(7)(iii)).
- Waiting on parts: OSHA’s November 2025 letter of interpretation allows non-lockout “continuity” or “out of service” locks while no employee faces exposure during servicing. Before work resumes, authorized employees verify isolation again and apply a compliant lockout or tagout device. OSHA sets no maximum time for leaving a lockout device on while awaiting parts.
- Annual inspection: Use the checklist as the reference when an authorized employee other than those using the procedure inspects it (29 CFR 1910.147(c)(6)(i)).
The best practices below cover LOTO inspections, training, and common mistakes.
Lockout/tagout best practices for compliance
Even the most experienced maintenance teams are occasionally tempted to take shortcuts. Best practices ensure that everyone fully follows lockout/tagout procedures and goes back home safe at the end of the day. Here are three LOTO best practices you should follow to ensure compliance and occupational safety:
Periodic inspections and recordkeeping
Audit your LOTO program at least once a year. Sooner if equipment is upgraded or procedures change.
During inspections, verify that:
- Locks and tags are in proper condition
- Isolation points are clearly marked
- Stored energy has been safely released
At every inspection, use a computerized maintenance management system (CMMS) to maintain detailed logs of which employees conducted the inspection, what devices were used, what anomalies were discovered, and what corrective action was taken.
For example, suppose the inspection records show that residual pressure remains in the hydraulic lines even after the machine is properly locked out. This pressure occasionally causes the press ram to drift slightly, which is a potential pinch hazard.
Since this record shows a recurring issue, you can proactively check if hydraulic lines have been fully bled to prevent injuries during future inspections.
Invest in training and enforcement
Hands-on training sessions help employees practice on the machines they’re going to maintain before they perform any maintenance.
For example, you can show them how to identify hidden energy sources, properly apply locks and tags, and release stored energy. You can also help them practice responding to scenarios that might arise. For instance, what if a co-worker forgets to remove a tag or equipment starts unexpectedly?
Combine training with clear enforcement. Communicate that sticking to lockout/tagout procedures is non-negotiable.
Verify compliance during audits and recognize teams or individuals who consistently follow protocols. And if you notice any near misses, treat them as opportunities to retrain workers.
Avoid common mistakes
Here are some common mistakes to watch out for:
- Skipping steps in the procedure to save time
- Assuming someone else has already locked or tagged the equipment
- Using makeshift devices (like zip ties) instead of proper lockout hardware
- Forgetting to release residual or stored energy
- Placing tags where they’re hard to see or easy to ignore
- Overlooking secondary energy sources on complex machines
Using a CMMS to manage LOTO procedures
Lockout/tagout is only effective if it’s consistent. However, consistency is tough when multiple teams (staff from different crews or shifts, or contractors) work on the same assets, or when procedures change because you installed new equipment.
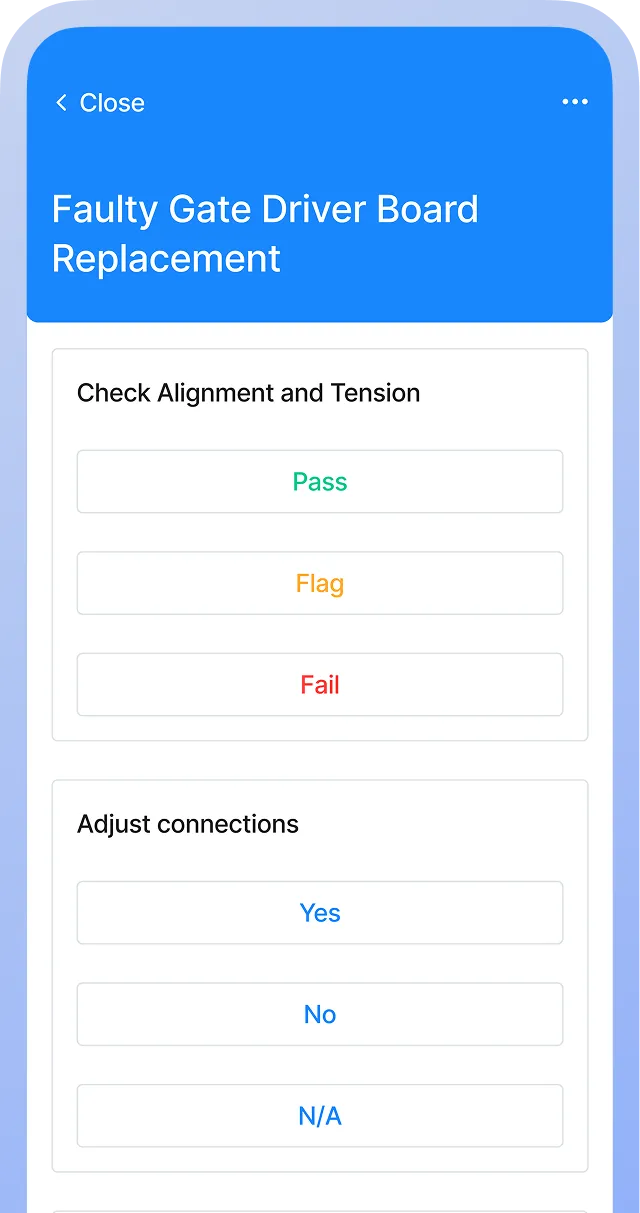
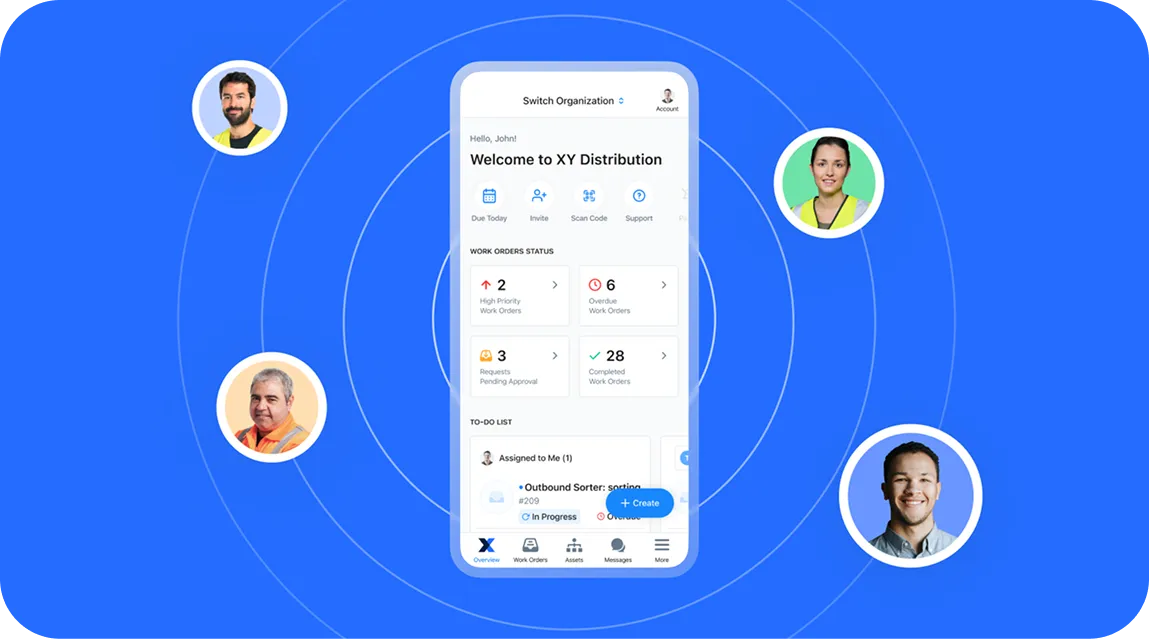
That’s where a CMMS can help. A CMMS lets you create standardized digital LOTO checklists, schedule periodic inspections, track training records, and document every lock and tag applied.
With a CMMS, your team doesn’t have to spend hours chasing paper logs. They can use their mobile devices to access data in a centralized system that keeps your LOTO program compliant and your workers safe.
If you’re ready to start implementing LOTO procedures and wave goodbye to compliance headaches, check out our comprehensive lockout/tagout guide.


LOTO procedure FAQs
What’s the best way to track and manage lockout devices across multiple sites?
The best way is to use a CMMS. A CMMS lets you assign devices to specific assets and standardize procedures across multiple locations. This reduces confusion, improves accountability, and ensures compliance with OSHA standards.
How can digital tools like safety software improve lockout/tagout recordkeeping and workflow?
Digital tools automate recordkeeping by logging lockout events and inspections in a centrally accessible digital location. They also streamline workflows with digital checklists and mobile access for technicians, speeding up audits and making compliance easier to prove.
What are the best practices for training employees on lockout/tagout responsibilities?
Here are some lockout/tagout training best practices:
- Tailor training for specific job roles
- Use real-world scenarios during training
- Conduct ongoing audits post-training
- Retrain team members after incidents
Marc Cousineau is the Senior Content Marketing Manager at MaintainX. Marc has over a decade of experience telling stories for technology brands, including more than five years writing about the maintenance and asset management industry.